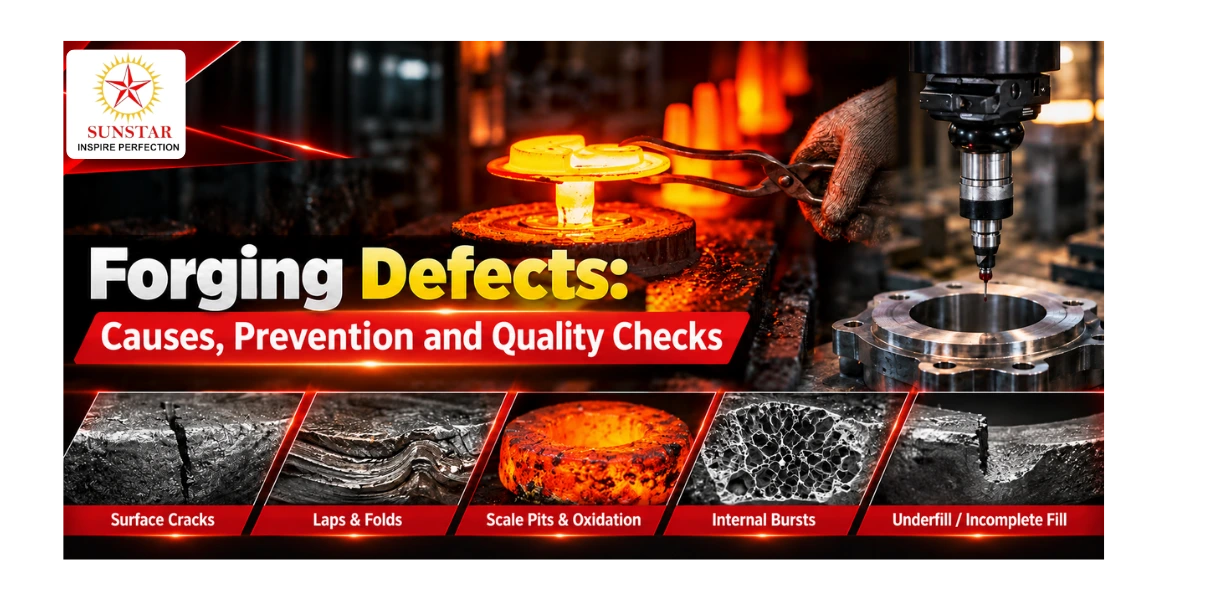
Forging defects are departures from the required shape, surface, internal soundness, dimensions or metallurgical condition of a forged component. They can originate in billet preparation, heating, die design, lubrication, deformation, trimming, heat treatment, handling or machining. Effective control therefore depends on the complete process route, not only final inspection.
The practical objective is prevention supported by detection. Manufacturers should translate drawings and customer requirements into process windows, maintain tooling and equipment, control material identity, monitor critical parameters, and use inspection methods suited to the defect risk. When a defect appears, containment is only the first step; the team must trace the mechanism and verify corrective action.
Classify the Defect Before Solving It
A useful classification separates surface defects, internal discontinuities, shape or fill problems, dimensional variation and metallurgical defects. The visible symptom may not reveal the true mechanism. A surface line could be a lap, crack, scale impression or machining mark, while low hardness may come from chemistry, heating, quenching or test preparation.
Define the defect using location, orientation, depth, frequency, heat or lot, die cavity, press, shift and process stage. Preserve samples and photographs. Avoid corrective actions based on labels alone; “crack” is not a root cause.
Common Defects and Immediate Questions
| Observed condition | Possible mechanisms | First checks |
| Underfill or unfilled section | Insufficient stock, low temperature, poor flow, inadequate energy | Billet weight, temperature, die fill, press data |
| Lap or fold | Metal flow folds over itself, poor preform or die radius | Flow line, preform, flash, lubrication |
| Surface crack | Low ductility, excessive strain, poor temperature or stress concentration | Temperature history, corner radii, material identity |
| Die shift or mismatch | Tool alignment, wear, seating or guide problem | Parting line, die setting, guide clearances |
| Scale pit | Oxide scale trapped against surface | Heating atmosphere, descaling and transfer time |
| Internal burst | Tensile stress, reduction sequence or billet condition | Sectioning, process simulation, reduction path |
Underfill and Incomplete Die Filling
Underfill appears when metal does not reach the intended cavity. Causes can include low billet mass, incorrect preform, insufficient forging temperature, poor lubrication, premature cooling, die wear, trapped gas, excessive flash resistance or inadequate press energy. The same symptom can have different causes across cavities.
Prevention begins with billet-weight control, verified heating, consistent transfer time, robust preform design and monitored press parameters. Compare defect position with flow direction. Repeated underfill at the same feature often points to local flow or venting; random occurrence may indicate material, temperature or loading variation.
Laps, Folds and Cold Shuts
A lap forms when material folds over and the interface does not weld completely. It may result from sharp preform transitions, excess material, poor die radii, unfavourable flow, scale or low interface temperature. Removing the visible line by machining may not remove the discontinuity below it.
Control the preform and deformation sequence so metal fills progressively without folding. Review die radii, gutter and flash design, billet placement and lubrication. Section trial parts at risk locations. When simulation is used, validate predictions against actual macrostructure and defect history.
Surface Cracks and Hot Tears
Surface cracking can occur when local strain exceeds material ductility. Low or excessive temperature, rapid cooling, sharp geometry, excessive reduction, material segregation, poor surface condition or incorrect steel grade can contribute. Cracks often align with stress and flow patterns, providing clues to origin.
Verify material certificates and positive identification where required. Review furnace uniformity, soak, transfer, deformation rate and die temperature. Improve radii or reduction sequence where strain concentrates. Do not weld-repair or blend a crack unless the approved specification and customer disposition explicitly allow it.
Internal Bursts and Central Discontinuities
Internal bursts can develop under unfavourable tensile stress within the workpiece even when the surface looks acceptable. Excessive reduction, poor die geometry, temperature gradients, billet defects and an unsuitable deformation path may contribute.
Risk evaluation can combine process design, simulation, macro-etching, ultrasonic examination and destructive validation. Prevention focuses on reduction sequence, temperature consistency, billet quality and tool geometry. Inspection must target the internal volume and orientation at risk.
Die Shift, Mismatch and Dimensional Variation
Mismatch appears across the parting line when upper and lower dies are not correctly aligned. Wear, damaged keys, guide clearance, poor seating, thermal effects and setup error are common contributors. Dimensional variation can also arise from stock variation, elastic deflection, incomplete fill, trimming and cooling distortion.
Use controlled setup verification, die identification, alignment checks and first-off approval. Trend dimensions by cavity and tool life rather than relying on pass/fail data alone. A gradual drift suggests wear or thermal change; a step change suggests setup, damage or process intervention.
Scale Pits, Oxidation and Surface Decarburisation
Heating in an oxidising atmosphere forms scale that can be pressed into the forging surface. Excessive temperature or time may increase oxidation and decarburisation. Poor descaling and long transfer expose the billet further.
Control furnace atmosphere, temperature, residence and transfer. Maintain descaling equipment and inspect nozzles or mechanical systems. Metallurgical examination can assess decarburisation where surface properties matter. Do not confuse removed scale with restored surface chemistry.
Flakes, Hydrogen Damage and Material-Related Risks
Flakes are internal cracks associated with hydrogen and residual stress in susceptible steels. Material cleanliness, section size, cooling and heat treatment influence risk. Other material-related concerns include segregation, inclusions, seams and mixed grades.
Use approved raw-material specifications, supplier controls, heat traceability and suitable thermal practice. Large or critical forgings may require controlled cooling or dehydrogenation treatment. Investigation should connect the discontinuity morphology and location with chemistry, process history and stress.
Heat-Treatment Defects
Quench cracks, distortion, soft spots, excessive hardness and non-uniform microstructure can arise after forging. Loading pattern, furnace uniformity, atmosphere, austenitising, transfer, quench severity, agitation and tempering all matter. Geometry and prior forging condition influence response.
Control recipes, instrument calibration, load configuration and quench condition. Measure hardness at defined locations and verify microstructure or mechanical properties when required. A hardness number alone cannot explain an abnormal result; correlate it with section, microstructure and treatment records.
Trim, Shot-Blast and Handling Damage
Trimming can create burrs, rollover or cracks when clearance, alignment or tool condition is poor. Shot blasting may reveal defects but can also affect the appearance of surface indications. Handling can create dents, impact marks and mixed lots.
Treat post-forging operations as controlled processes. Define tool condition, media, exposure, handling containers and identification. Inspect at logical gates so the origin stage can be narrowed when damage appears.
Design Prevention into Process Planning
Sunstar states that its route combines design support, tool and die development, forging, heat treatment, machining, finishing and inspection. Review its forging and machining capabilities as context for an integrated control plan. The component-specific plan should still define material, flow, reduction, temperatures, dies, equipment, sampling and acceptance.
Use drawing review and feasibility analysis to identify sharp transitions, thin ribs, machining allowance, grain-flow expectations and inspection access. Develop the billet and preform sequence around controlled metal flow. Confirm capacity and energy, not merely press nameplate tonnage.
Control the Process Window
Critical parameters may include billet weight, cut length, furnace zone temperature, soak time, transfer time, die temperature, lubricant concentration, press energy or stroke, flash condition and cooling route. Define target, tolerance, method, frequency, reaction plan and record owner.
A control limit should trigger a response before defects accumulate. Stop, segregate and verify when process evidence is outside the approved window. Do not retrospectively adjust records to match accepted parts.
Select Inspection Methods by Failure Mode
Sunstar’s driveline component page describes visual and dimensional checks, surface and internal NDT, mechanical testing and metallurgical examination. Method selection must follow drawing, standard, customer and risk requirements; no single method finds every defect.
Visual inspection can identify surface condition and gross fill problems. Magnetic-particle inspection suits surface and near-surface discontinuities in ferromagnetic materials; dye penetrant can reveal surface-breaking discontinuities in suitable non-porous materials. Ultrasonic or radiographic techniques may address internal risks, subject to geometry, sensitivity and procedure qualification.
Dimensional inspection verifies shape, position, runout, threads and surface finish. Hardness, tensile, impact, macro and micro examinations address properties and structure. Ensure personnel qualification, equipment calibration, reference standards, coverage and acceptance criteria are documented.
Investigate Defects with Evidence
- Contain the affected heat, lot, cavity and subsequent processing without destroying traceability.
- Describe the defect and reproduce its location with photographs, sections and measurements.
- Compare good and defective parts, process records, tooling condition, material data and shift events.
- Test the most likely mechanism through targeted trials; change one controlled factor where practical.
- Verify corrective action over enough production to show stability, then update controls, training and documents.
Quality-Control Checklist for Forged Components
- Material identity and heat traceability are intact.
- Billet dimensions and weight meet the approved plan.
- Heating, transfer and die conditions are within the window.
- Tool setup, alignment, lubrication and wear checks are recorded.
- First-off and in-process inspections cover critical characteristics.
- NDT, mechanical and metallurgical tests match the risk and specification.
- Nonconforming material is segregated with clear disposition authority.
- Corrective actions are verified through data, not closure dates alone.
Use Tool-Life and Maintenance Data
Tooling condition affects fill, flash, mismatch, surface quality and dimensions. Record die set, cavity, production count, repair history and observed wear. Link defect data to tool life so maintenance is triggered by evidence before the process drifts beyond acceptance. A total shot count without cavity-level history can hide a local problem.
After die repair, treat the first production as a controlled restart. Verify seating, alignment, dimensions, surface condition and process parameters. Preserve repair details and changes to radii, vents or flash land. Unrecorded polishing and local rework can alter metal flow and make later investigation difficult.
Set a Risk-Based Sampling Strategy
Sampling should reflect defect severity, process capability, detection reliability, production volume and customer requirements. Critical characteristics may require higher frequency or automated inspection, while stable characteristics can follow a validated sampling plan. First-off approval does not justify ignoring drift during a long run.
Define the reaction when one sample fails: stop point, containment boundary, additional inspection and restart approval. Use cavity, heat and time sequence to establish the suspect population. Randomly checking more parts without a containment rule can create activity without controlling risk.
Connect Supplier and Customer Quality Evidence
Agree drawing interpretation, defect terminology, inspection method, acceptance criteria, sample submission and change control before production. A surface condition acceptable before machining may be unacceptable on the finished functional area. Record which party owns each verification step and which documents accompany the shipment.
When a customer reports a defect, request part identity, lot, photographs, location, operating context and inspection method. Protect the customer while evidence is gathered. Avoid declaring operator error, material fault or design weakness before the mechanism is demonstrated. Clear technical communication shortens containment and prevents repeated argument.
Measure the Cost of Poor Quality
Defect cost includes more than scrap. Add sorting, rework, tool damage, furnace and press time, delayed delivery, premium freight, customer disruption, investigation and lost capacity. Separating these costs by defect family helps management fund prevention where it has the greatest operational effect.
Balance yield improvement with risk. Reducing flash, inspection or process margins can lower cost only when capability and failure consequences are understood. Sustainable improvement removes the defect mechanism while maintaining required properties, traceability and customer confidence.
Use Capability Data without Hiding Defect Mechanisms
Process-capability indices can summarise dimensional stability when the process is controlled and the distribution assumptions are appropriate. They do not prove the absence of cracks, laps or internal discontinuities. Review measurement-system performance and control charts before interpreting a capability number.
Stratify data by cavity, die set, heat, machine and shift. A combined result can appear acceptable while one cavity drifts. Use attribute data for defect occurrence and variable data for measurable characteristics, then connect both to the process parameter and maintenance history.
Plan the Launch of a New Forged Component
A controlled launch should include feasibility review, process flow, PFMEA, control plan, tooling approval, material plan, trial protocol, measurement-system analysis, capability evidence and sample submission as required by the customer. Define temporary heightened inspection until process evidence supports normal production controls.
Record deviations and lessons from each trial. Confirm that production tooling, equipment, operators, material and inspection methods match the intended serial process. A successful hand-made sample does not demonstrate repeatable volume capability if normal conditions are different.
Maintain Traceability through Machining and Heat Treatment
Forgings may be mixed, split or combined as they move through heat treatment, shot blasting and machining. Define lot identity at every transfer and preserve the link to material heat, forging run, die cavity and inspection records. Marking methods must remain legible without damaging the component.
When a nonconformance is discovered late, traceability determines whether containment is precise or unnecessarily broad. Test the system periodically by selecting a finished component and reconstructing its route, then selecting a raw-material heat and identifying all affected finished lots.
Include subcontracted operations in the same traceability logic. Purchase orders and job cards should define identification, records, preservation, return status and notification of deviations. Incoming verification must confirm that outsourced processing did not break the component history or approved route.
Audit one complete outsourced lot periodically and close any traceability gap before the next dispatch.
Frequently Asked Questions
1. What is the most common forging defect?
Frequency varies by component and process. Underfill, laps, cracks, scale pits and mismatch are common categories, but actual data should guide priorities.
2. What causes underfill in closed-die forging?
Possible causes include insufficient stock, low temperature, poor preform or flow, die wear, trapped gas, lubrication variation and inadequate equipment energy.
3. What is the difference between a lap and a crack?
A lap is a folded interface created by metal flow; a crack is a fracture caused when stress exceeds local ductility or strength. Examination may be needed to distinguish them.
4. Can forging defects be removed by machining?
Only if the approved machining allowance completely removes the condition and the specification permits it. Subsurface discontinuities must not be assumed away.
5. How are internal forging defects detected?
Ultrasonic, radiographic or destructive sectioning methods may be used depending on material, geometry, orientation, sensitivity and requirements.
6. Why do scale pits occur?
Oxide scale can form during heating and become pressed into the surface when atmosphere, time, temperature, descaling or transfer is poorly controlled.
7. What causes die mismatch?
Misalignment, wear, damaged guides or keys, poor seating, setup error and thermal effects can shift the die halves.
8. Can hardness testing prove a forging is defect-free?
No. Hardness addresses a property at tested locations; it does not replace dimensional, surface, internal or metallurgical inspection.
9. How does grain flow relate to quality?
Controlled grain flow can support component performance, but it must be evaluated against design and process requirements. Poor flow may indicate an unsuitable preform or deformation route.
10. When is magnetic-particle testing suitable?
It is used for surface and near-surface discontinuities in ferromagnetic materials under a qualified procedure.
11. What should happen when a defect is found?
Contain affected material, preserve traceability, characterise the defect, investigate the mechanism, disposition through authorised review and verify corrective action.
12. How can buyers evaluate a forging supplier’s defect control?
Review process planning, traceability, control plans, equipment, tooling, inspection capability, personnel qualification, nonconformance control and evidence of corrective-action effectiveness.
Reduce Forging Defects by Controlling the Entire Manufacturing Route
Reliable forgings come from aligned design, material, tooling, heat, deformation, treatment, machining and inspection controls. Review Sunstar Precision Forge Limited’s profile and relevant component capabilities, then use the Sunstar contact page to share your drawing, material grade, annual volume, critical characteristics, testing requirements and delivery programme for a manufacturing feasibility discussion.